The Ultimate Guide to Box Dielines: Engineering the Perfect Cut
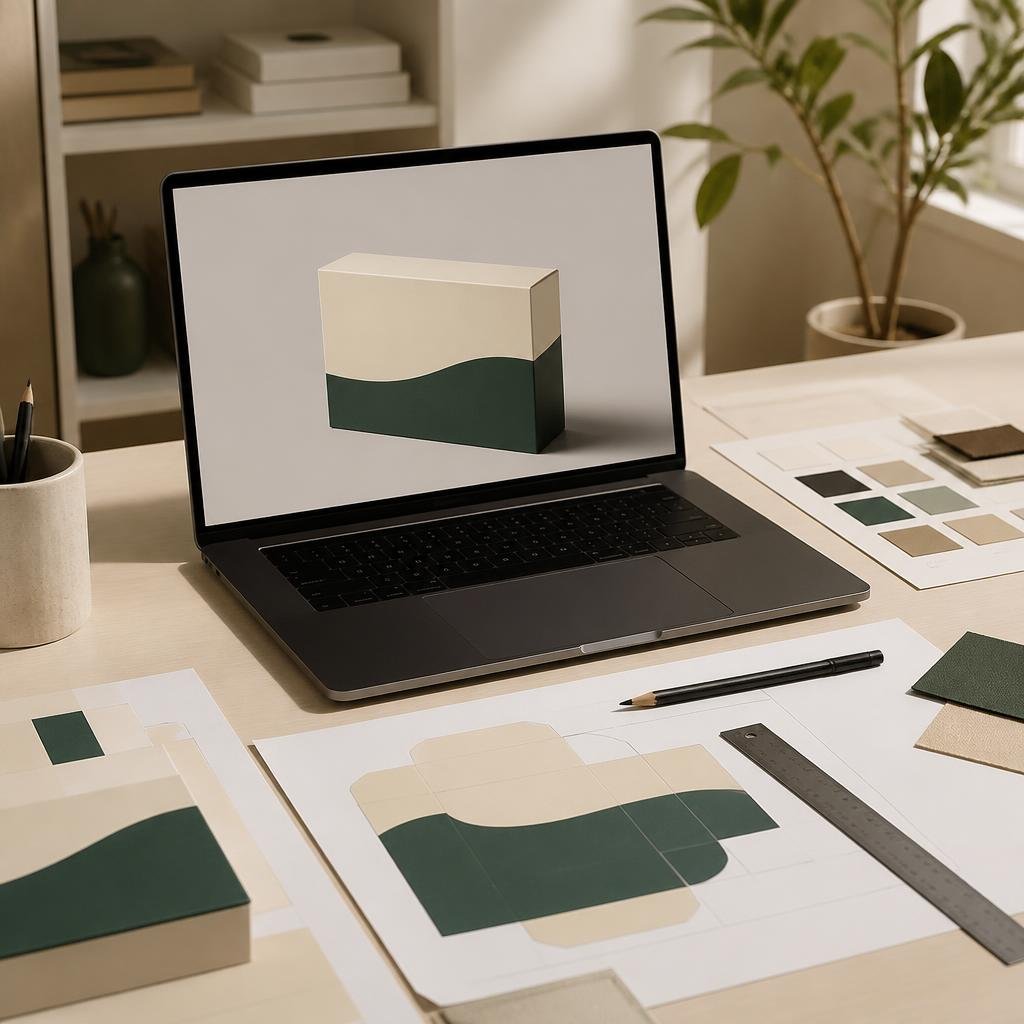
A dieline is the fundamental architectural blueprint of any physical box packaging project. It is the master vector file that dictates exactly where a commercial die-cutting machine will slice through the paperboard, where it will press a folding crease, and where the factory will apply the structural glue. Without a mathematically perfect dieline, a commercial print run will fail catastrophically.
Understanding the Vector Mechanics
Unlike standard graphic design, which relies on pixels, dieline engineering operates entirely in mathematical vectors. Commercial die-making machinery—such as laser cutters and automated rule-benders—cannot read JPEGs or PNGs. They require continuous, un-broken vector paths (typically supplied as Adobe Illustrator .AI or AutoCAD .DXF files). If a designer leaves a microscopic 0.1mm gap between two line segments, the laser cutter will stop immediately, resulting in machine downtime and factory rejection.
The Three Primary Line Types
Every commercial dieline utilizes a strict color-coding system to separate mechanical actions on the printing press:
- Solid Red Lines (Cut Lines): These dictate where the steel-rule die will physically slice completely through the paperboard or corrugated material.
- Dashed Green Lines (Crease/Score Lines): These dictate where the die will press a blunt steel rule into the board, crushing the fibers to create a hinge that allows the box to fold without the paper cracking.
- Blue Dashed Lines (Perforation): These dictate a zip-tear or tear-away opening mechanism.
Calculating Material Caliper and Offset
The most common error amateur designers make when drawing a dieline is ignoring the physical thickness (caliper) of the material. Paperboard is not a two-dimensional object; it occupies physical space. When you fold a piece of 24pt (0.6mm) SBS board or a piece of 3.0mm B-flute corrugated cardboard, the material wraps around an axis.
If you have an interior dust flap designed to fold inside an outer wall, you cannot make both flaps exactly 2.0 inches wide. The inner flap must be mathematically offset (reduced in width) by exactly the thickness of the board multiplied by two, plus a micro-tolerance for the hinge radius. If this deduction is not calculated into the vector dieline, the inner flap will crash into the outer wall during assembly, causing the entire box lid to bow outward.
Bleed and Safety Margins
Industrial die-cutting is an incredibly violent, high-speed physical process. As sheets of paperboard race through the press at 5,000 sheets per hour, there will always be a mechanical shifting tolerance of roughly 1mm to 2mm. To compensate for this shifting, the dieline must include a "Bleed" margin.
A Bleed requires the graphic designer to extend all background colors and pattern artwork at least 0.125 inches (3.175mm) past the solid red cut line. This ensures that if the die blade shifts slightly outward, it cuts into printed color rather than exposing a glaring white paper edge. Conversely, the "Safety Margin" requires all critical text (like FDA ingredient panels and barcodes) to be placed at least 0.125 inches inward from any cut or crease line, ensuring it isn't sliced off or rendered illegible by folding tension.
Glue Flap Angles and Machine Compatibility
For folding cartons (like a standard Straight Tuck box), the manufacturer relies on automated high-speed folder-gluers. The glue flap cannot simply be a straight rectangle. The top and bottom corners of the glue flap must be chamfered (angled), typically at exactly 45 degrees. If they are not angled, the sharp corners of the flap will catch on the high-speed belts of the gluing machine, ripping the box to shreds and jamming the production line.
Topic FAQs
No. Photoshop is a raster-based (pixel) program. Dielines must be engineered in vector-based software like Adobe Illustrator (.AI), CorelDRAW, or dedicated CAD software like Esko ArtiosCAD to ensure factory machines can read the mathematical paths.
The global standard for commercial box printing bleed is 0.125 inches (1/8th of an inch) or 3mm extending beyond the structural cut line.
The box will fail to close. The interior flaps will crash into the exterior walls, causing the box structure to warp, bow, or tear when physically assembled.